Sheet and section cutting
It is the first step in almost any part and it sets everything that follows: a clean cut saves work in bending, welding and finishing. We cut up to 10 mm thick in two ways, depending on the material and the geometry.
Up to 10 mm thick
That is our cutting limit in the workshop and it applies to all four materials. If your part needs more thickness, tell us anyway: some projects are solved by combining thicknesses rather than moving to a single thicker sheet.
Shearing
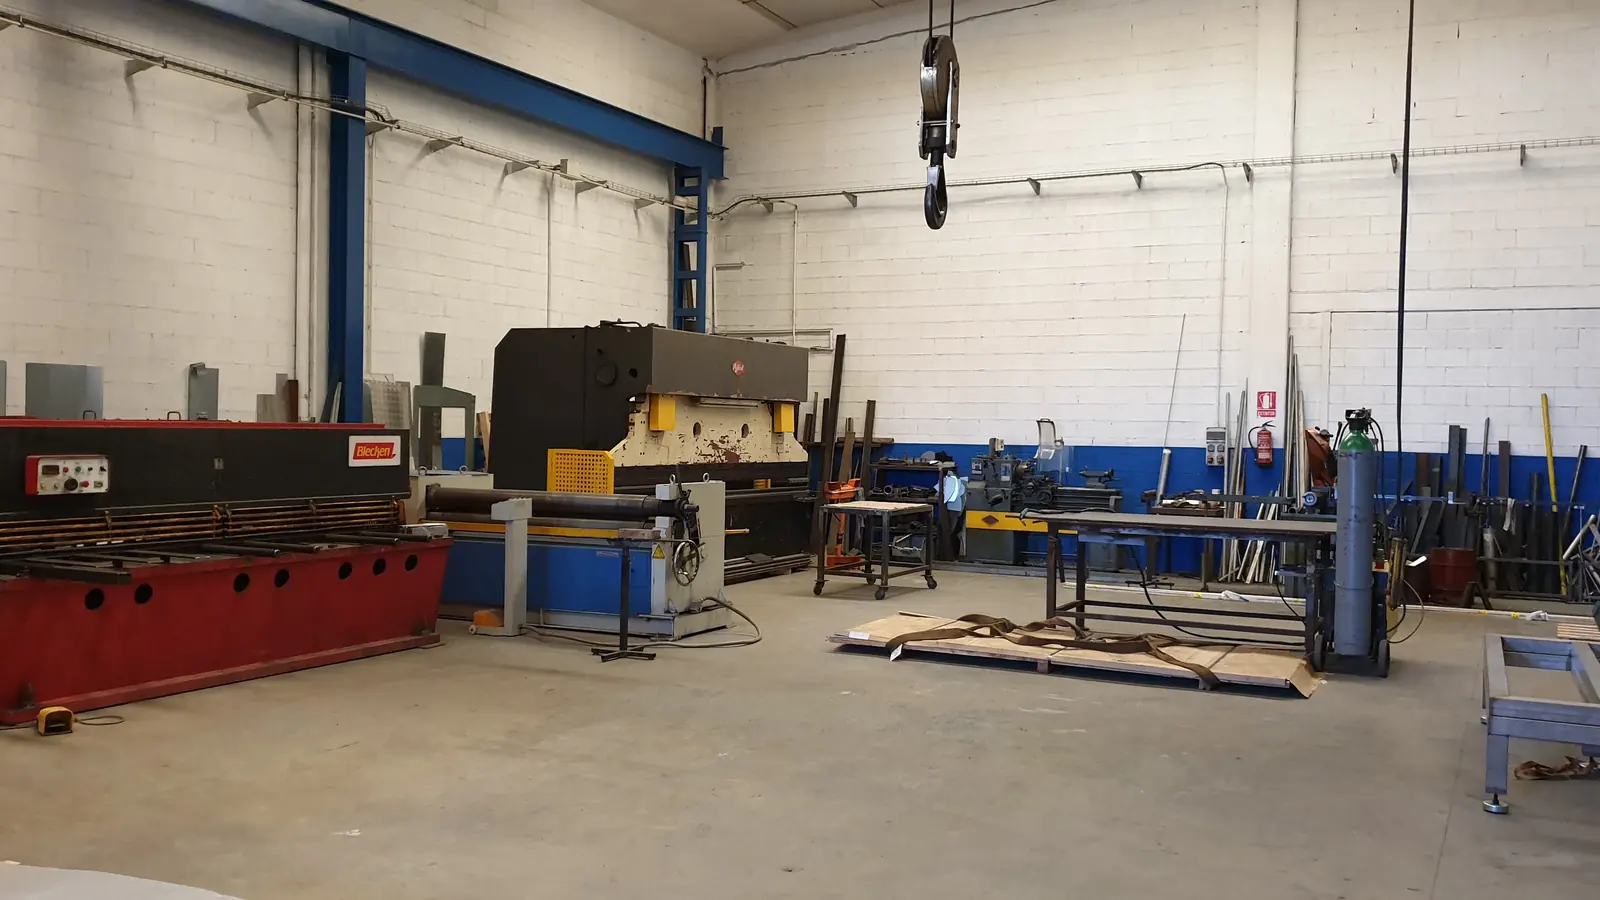
For sheet, in straight cuts. It is fast, generates no heat and does not alter the material at the edge, which matters in stainless steel: there is no heat-affected zone to worry about afterwards.
It is the default option when many identical parts have to be cut from a sheet and the cut is straight.
Bandsaw cutting
For sections, tube and solid bar, and for anything the shear cannot take. It allows mitre cuts and prepares the rolled sections that then go to the section bender or straight to welding.
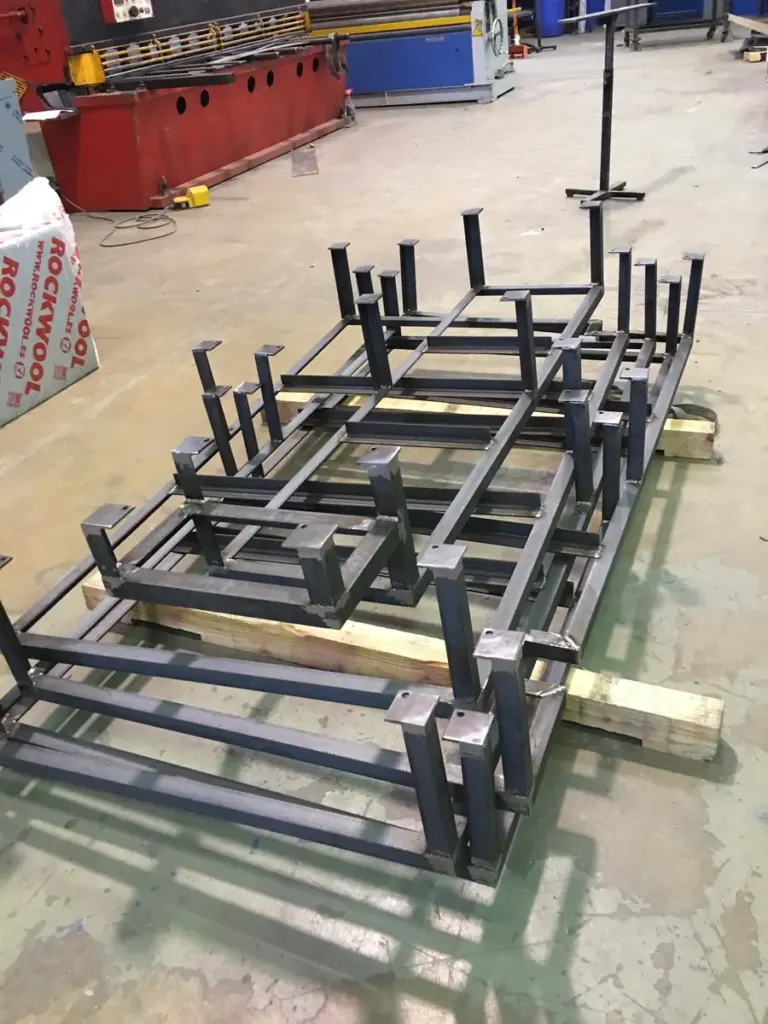
This is the cut we use to prepare structures, machine bases and tubular frames before assembly.
Materials
Stainless steel, mild steel, galvanised steel and aluminium. These are the four materials we work with in all our processes.
70% of what leaves our workshop is stainless steel, so that is where we have the most experience. But your project need not be limited to it: many parts combine stainless with mild or galvanised steel, depending on the function of each section.
When it ends here and when it continues
Some clients ask us for cutting only, with their own sheet or with material we supply. In other projects cutting is step one of six. Both are normal work for us.
Quotation
Send us your cutting list
With the drawing or dimensioned sketch we will tell you whether it suits the shear or the saw and prepare your quotation.